Elegir entre una máquina de marcado láser UV de 3 W, 5 W y 10 W no se trata simplemente de comprar más potencia láser. La elección correcta es la máquina que produce una marca aceptable en su material, cumple con el tiempo de ciclo de su producción y proporciona un margen de proceso suficiente sin costos innecesarios de equipo.
Para marcas pequeñas y detalladas con requisitos de producción modestos, un láser UV de 3 W puede ser suficiente. Conviene evaluar una máquina de 5 W cuando la potencia adicional pueda reducir el tiempo de procesamiento o mejorar la ventana de proceso utilizable. Un sistema de 10 W merece consideración cuando la carga de trabajo de marcado es mayor y las pruebas demuestran que la potencia adicional aporta un beneficio de producción significativo.
Estos son puntos de partida, no límites fijos de aplicación. Un láser de 10 W no produce automáticamente una marca más nítida ni funciona tres veces más rápido que un láser de 3 W. La fuente láser, las características del pulso, la óptica, el material, el patrón de marcado y las condiciones de producción influyen en el resultado.
| Potencia del láser UV | Cuándo considerarlo primero | Qué verificar |
|---|---|---|
| 3W | Marcas pequeñas, detalles finos y cargas de marcado moderadas | Contraste, detalle, repetibilidad y tiempo de ciclo requeridos |
| 5W | Aplicaciones que necesitan más margen de procesamiento o potencialmente menor tiempo de marcado | Mejora medible respecto a un proceso de 3W aceptable |
| 10W | Cargas de marcado mayores, patrones rellenos más grandes o ciclos de producción exigentes | Ganancia real de rendimiento sin daños inaceptables en el material |
El método de selección más fiable consiste en definir sus requisitos de marcado, comparar configuraciones de máquina adecuadas y validar las candidatas con muestras representativas.
¿Qué debe comprobar antes de elegir la potencia del láser UV?
Antes de comparar la potencia en vatios, identifique qué debe lograr la máquina. Puede que dos fabricantes necesiten marcar componentes de plástico, pero uno puede requerir un pequeño número de serie cada pocos minutos, mientras que el otro debe producir códigos legibles en una línea de producción en movimiento. Son problemas diferentes de selección de equipos.
Material, estado de la superficie y límites de daño
El marcado con láser UV suele utilizar una longitud de onda de 355 nm. Su interacción con muchos plásticos, recubrimientos y superficies sensibles lo hace útil para aplicaciones en las que el marcado con láser infrarrojo convencional puede causar efectos térmicos excesivos. Sin embargo, el marcado UV no está automáticamente exento de calor ni de daños en el material. La respuesta depende de la pieza de trabajo real.
En el caso de los componentes de plástico, el grado de polímero, los pigmentos, las cargas, los aditivos, la textura superficial y las condiciones de moldeo pueden afectar el contraste de la marca y el comportamiento de procesamiento. Dos piezas descritas simplemente como “ABS” o “policarbonato” pueden requerir ajustes diferentes.
El vidrio introduce otras consideraciones. Es posible que se pueda lograr una marca visible, pero la modificación excesiva de la superficie, el microagrietamiento, el astillamiento o la pérdida de integridad mecánica pueden ser inaceptables.
Antes de seleccionar la potencia, confirme:
- El material o la formulación exactos, cuando estén disponibles.
- Color de la superficie, recubrimiento, acabado y espesor.
- Si la marca debe ser oscura, clara, esmerilada o visualmente distinta de otro modo.
- Si se permite la fusión, la decoloración, el agrietamiento o la deformación superficial.
- Cualquier limpieza, abrasión, exposición química o proceso posterior que la marca deba soportar.
La descripción del material por sí sola no puede establecer si 3W, 5W o 10W serán suficientes. Para obtener una explicación más amplia del proceso, consulte nuestra Guía de tecnología de marcado con láser UV.
Tamaño de la marca, detalle y calidad requerida
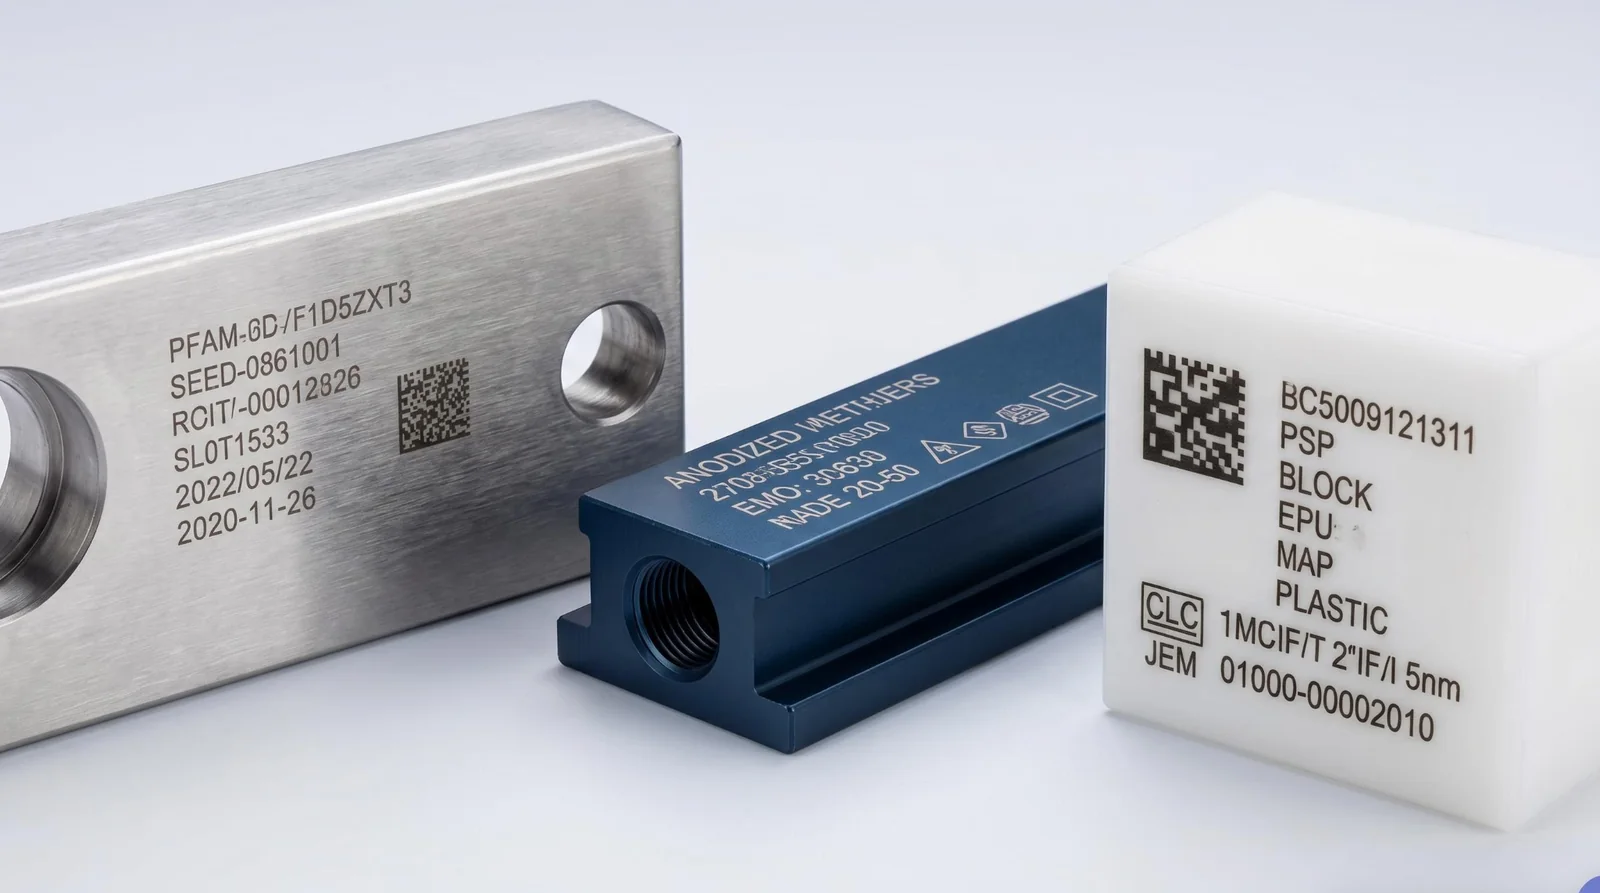
Un número de serie pequeño y un logotipo grande relleno pueden generar cargas de trabajo láser muy diferentes, incluso cuando aparecen sobre el mismo material. Un contorno pequeño puede requerir un procesamiento limitado, mientras que un diseño relleno implica muchas líneas de escaneo muy próximas entre sí. Aumentar el área rellena, el contraste requerido o el número de pasadas puede incrementar el tiempo de marcado.
Los criterios de aceptación deben definirse antes de las pruebas. Para texto y gráficos, las comprobaciones útiles incluyen la legibilidad de los caracteres, la definición de los bordes, la uniformidad del relleno y los cambios superficiales no deseados.
Para códigos QR o símbolos Data Matrix, la apariencia visual por sí sola no es suficiente. El código debe cumplir las condiciones de lectura requeridas, incluidos su tamaño real, el contraste, la superficie circundante y el lector previsto. Si la pieza tiene un recubrimiento delicado, el cambio superficial aceptable puede importar más que el grado de oscuridad de la marca.
Un láser de mayor potencia no proporciona por sí mismo detalles más finos. El punto enfocado, la calidad del haz, la lente de campo, la precisión de escaneo y la respuesta del material también determinan lo que la máquina puede producir.
Volumen de producción y tiempo de ciclo disponible
La demanda de producción suele ser la razón por la que los compradores consideran una potencia láser UV mayor. Sin embargo, la producción diaria y el tiempo de marcado láser no son la misma medida.
El ciclo de producción completo puede incluir posicionamiento, carga, enfoque o ajuste de altura, marcado, verificación de código y descarga. Cuando estas operaciones dominan el ciclo, reducir el tiempo con el láser encendido puede aportar poca mejora a la producción real.
Una estación de trabajo que produce pequeñas marcas de identificación por lotes puede tener tiempo suficiente para completar cada marca con un sistema de 3 W. Una estación de producción con una ventana de marcado corta puede requerir una capacidad de procesamiento diferente, incluso cuando la marca en sí es relativamente pequeña.
La pregunta relevante no es simplemente qué tan rápido puede moverse el escáner. Se trata de si el sistema completo puede producir de forma consistente piezas aceptables dentro del tiempo de ciclo disponible.
Prepare una ficha básica de marcado que contenga el material, el diseño, el tamaño de la marca, los criterios de aceptación, el volumen de producción esperado y el tiempo de ciclo objetivo. Estos detalles hacen que la comparación de potencias sea significativa.
¿Qué cambia realmente entre los láseres UV de 3 W, 5 W y 10 W?
La potencia en vatios en las especificaciones de un láser UV normalmente se refiere a potencia media de salida óptica nominal en condiciones de funcionamiento definidas. No representa la potencia eléctrica consumida por la máquina completa, ni describe completamente la energía entregada por pulsos individuales.
Diferencias entre potencia media, energía de pulso y fuente láser
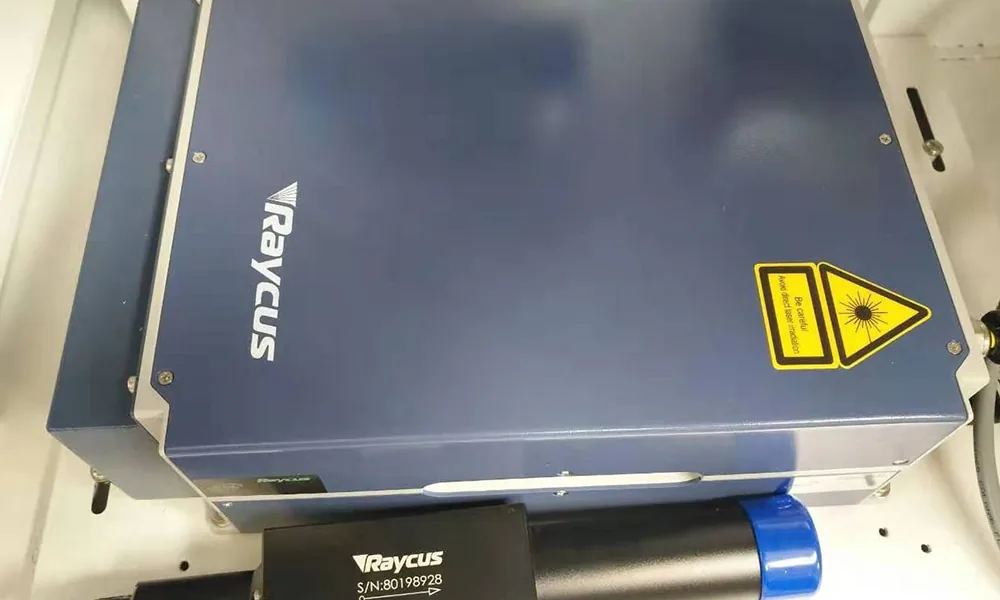
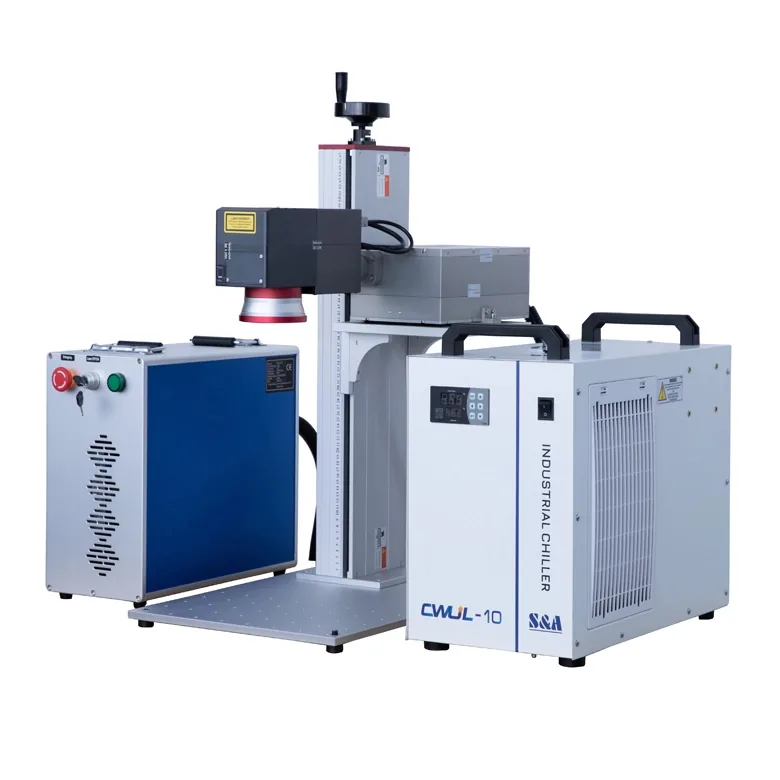
Muchos sistemas industriales de marcado UV utilizan fuentes láser de estado sólido pulsadas y bombeadas por diodo. Su rendimiento depende de algo más que la potencia de salida nominal.
La frecuencia de repetición de pulsos indica con qué frecuencia se emiten los pulsos. En las condiciones de funcionamiento pulsado aplicables, la energía media por pulso es aproximadamente la potencia óptica media dividida por la frecuencia de repetición. La anchura de pulso, la calidad del haz y el comportamiento potencia-frecuencia del láser también afectan al procesamiento. Es posible que la fuente no mantenga su potencia de salida nominal en todo el intervalo de frecuencias.
Los datos del fabricante ilustran por qué importa el modelo exacto. A continuación se presenta una selección de especificaciones de fuente láser UV JPT, no cifras de rendimiento medidas para máquinas de marcado completas ni para las configuraciones estándar suministradas por Zhuorui Laser.
| Modelo de fuente láser | Condición de salida publicada | Rango de frecuencia de repetición indicado | Refrigeración de la fuente |
|---|---|---|---|
| >3 W a 30 kHz | 20–200 kHz | Refrigerado por agua | SEAL-355-3E |
| >5 W a 40 kHz | SEAL-355-5E | Refrigerado por agua | SEAL-355-3E |
| >10 W a 60 kHz | SEAL-355-10S | 40–300 kHz | SEAL-355-3E |
Sources: JPT’s SEAL 355-3/5 specifications y SEAL 355-10/15/20/30 specifications. The figures describe the listed laser sources at specified conditions; they do not establish proportional marking-speed differences.
Cooling also varies by source family. For example, JPT’s LARK 355-3/5 series includes air-cooled 3W and 5W models, while the SEAL models in the table use water cooling. The complete machine must be configured for its installed laser source.
Marking Speed and Available Processing Margin
Additional laser power can be useful when the current process is limited by the energy available for an acceptable mark.
Consider a filled pattern that requires multiple passes to reach the specified contrast. Under suitable material and laser conditions, a higher-power system may support a different combination of scan speed, repetition frequency, and passes that reduces total marking time.
That improvement is not guaranteed. The material may not tolerate additional energy deposition; the source may deliver its rated power at a different pulse frequency; or the scanner, focusing conditions, and production handling may already be limiting the cycle. Doubling average laser power therefore does not mean doubling accepted production output.
Processing margin also matters. A machine that produces a good result only within a very narrow parameter range may be less suitable for production than one that maintains the required result across realistic variations in material and operation.
A useful power upgrade should improve at least one relevant outcome: accepted marking speed, usable process margin, or the ability to meet an otherwise difficult marking requirement.
Why Higher Power Does Not Automatically Mean Better Quality
The best-looking mark is not necessarily produced at the highest available power.
On a heat-sensitive polymer, excessive energy concentration may cause discoloration, melting, raised edges, or other unwanted changes. On glass, the process may need careful control to limit cracking and surface damage. Conversely, a higher-rated laser operated within a suitable process window is not automatically less precise than a lower-power model.
The relevant factors include the focused spot and optical system; pulse characteristics and energy distribution; scan speed, pulse overlap, and hatch spacing; material absorption and thermal response; and focus variation across the marking field.
When precision is the dominant requirement, compare the actual marks under the intended inspection conditions rather than treating wattage as a substitute for quality. For a broader explanation, see why laser power is not the only factor.
Which UV Laser Power Should You Test for Your Application?
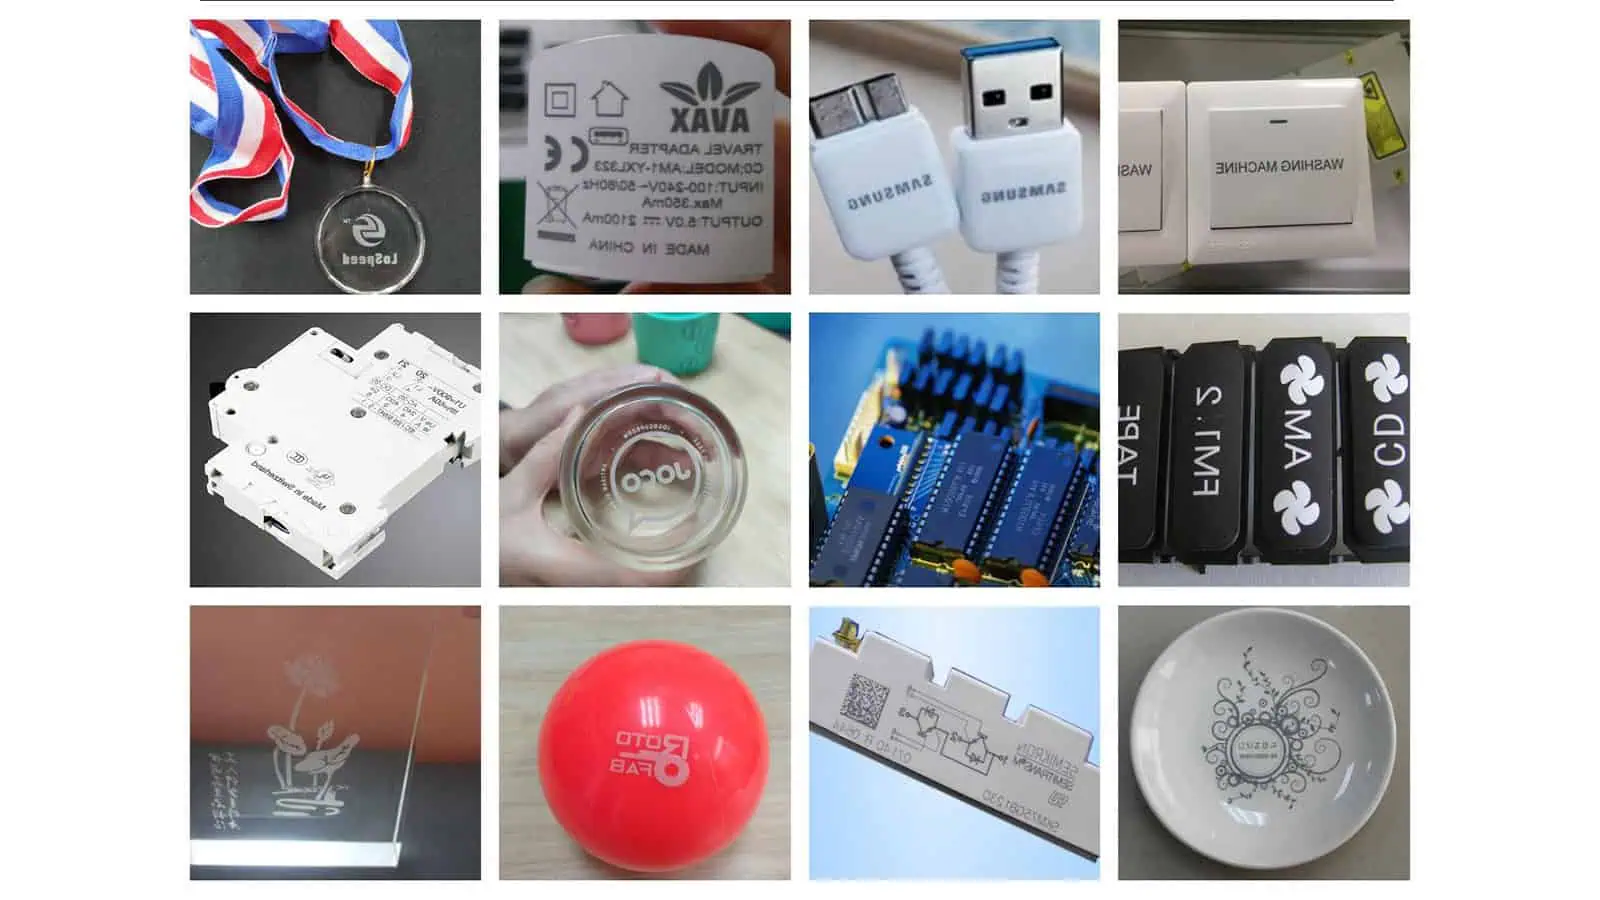
The most useful way to shortlist UV power is to consider the marking task rather than assign a fixed wattage to every material. The following matrix suggests initial testing directions, not material-compatibility guarantees.
| Tarea de marcado | Candidate comparison | Main acceptance question |
|---|---|---|
| Small characters or compact identification marks | Begin with 3W; compare 5W if needed | Does the mark meet quality and cycle-time requirements? |
| Routine plastic-part coding | Compare 3W and 5W | Does additional power improve accepted output? |
| Larger filled logos or demanding marking workloads | Compare 5W and 10W; retain a 3W baseline when useful | Is time reduced without unacceptable surface changes? |
| Glass or other damage-sensitive surfaces | Select candidates after reviewing the material and mark | Can the required effect be achieved without unacceptable defects? |
| Short marking windows or moving-part coding | Test power together with motion and control configuration | Can the complete system maintain quality at production speed? |
Three illustrative engineering scenarios show how these decisions differ. They are examples of selection logic, not recorded customer tests or measured Zhuorui Laser results.
Scenario 1: Fine identification marks on an electronic plastic housing. Suppose a molded housing requires a compact serial number or Data Matrix symbol without damaging the surrounding plastic. Begin by checking whether a 3W UV system can produce an acceptable mark within the available cycle time. If it can do so repeatedly with sufficient process margin, more power may offer little benefit. If quality is acceptable but the processing time is too long, comparing a suitable 5W configuration becomes reasonable. Judge both the code readability and surface condition, not simply which sample looks darker.
Scenario 2: A larger filled logo on a coated polymer component. A filled design may require substantially more scan coverage than a few small characters. Depending on the coating and target appearance, a 5W system may complete the accepted pattern faster than a 3W machine. If the required cycle time remains out of reach, a suitable 10W candidate can be tested. Check coating integrity, edge quality, uniformity, and whether the supposed speed improvement remains when only acceptable results are counted.
Scenario 3: Variable-data coding at a production station. A manufacturer may need changing codes within a short available marking window. If laser-on time is the verified bottleneck, comparing higher power could be justified. If the constraint comes from part positioning, trigger timing, data handling, or motion, increasing laser power will not correct the underlying cause. A machine-side review should cover marking time, positioning, control signals, data content, and verification. Flying or online marking needs configuration-specific confirmation.
Similar-looking applications may therefore justify different power choices. The actual acceptance requirement—not the material name or wattage alone—controls the shortlist.
When Is a 5W or 10W UV Laser Worth the Extra Cost?
A higher-power UV laser marking machine may cost more, but the difference between quotations is not determined by laser power alone. The more useful question is whether the proposed configuration delivers enough additional value for the actual application.
Compare Complete Machine Configurations, Not Wattage Alone
Two machines with similar cabinets and the same advertised power may contain different laser sources, optics, cooling systems, controllers, and accessories. Before comparing prices, request quotations that clearly identify:
- Fuente láser: Brand, exact model, rated operating conditions, and supported parameters.
- Marking optics: Galvo scanner, field lens, marking area, and working-distance requirements.
- Cooling: Air- or water-cooled configuration and any supporting equipment required.
- Controles: Software, controller, variable-data functions, and required interfaces.
- Workpiece handling: Fixtures, positioning aids, and any installed rotary or vision functions.
- Seguridad y extracción: Actual enclosure, interlocks, and fume-control provisions.
- Delivery scope: Computer, accessories, commissioning, documentation, spare parts, and support terms.
A 5W quotation with a better-matched optical system and more suitable machine configuration may be more valuable than a nominally higher-powered system with the wrong marking field or missing production requirements. A cooling system or optional module should be evaluated as part of the actual equipment package, not assumed to be included because of wattage.
Compare Upgrade Cost Against Accepted Production Output
Power upgrades become easier to justify when they solve a measurable production problem. If a 3W machine produces acceptable marks at the required output rate, a 5W option may not generate enough additional value to justify its cost.
When an acceptable 3W process cannot meet the production target, test whether a 5W configuration improves the completed process sufficiently. A 10W system becomes attractive when the additional output is usable, the material remains within acceptable limits, and the gain matters to production.
Compare accepted parts produced over the required operating period, changes in complete cycle time, rejected marks and rework, recurring operating costs, and any justified need for future capacity. Higher power only adds useful capacity if the process can actually benefit from it.
There is no reliable universal price premium or payback period for moving from 3W to 5W or 10W. Those figures require specific equipment quotations and validated operating data.
How to Compare 3W, 5W, and 10W UV Lasers in a Sample Test
A sample test should answer a purchasing question, not merely demonstrate that a laser can leave a visible mark. The purpose is to determine which proposed configuration meets the same production requirements at an acceptable cost.
Use Representative Workpieces and the Same Acceptance Criteria
Use production-representative samples wherever possible. If the material has multiple grades, finishes, colors, or coatings, include the variations that could change marking behavior.
Each candidate should be evaluated against the same required task: identical marking content and intended dimensions; the same quality and readability criteria; applicable surface-damage limits; production cycle-time requirements; and comparable inspection methods.
For a Data Matrix code, compare whether each candidate produces an acceptable, readable symbol under the intended reader and inspection conditions. A visually darker symbol should not automatically be considered better if its geometry or surrounding material is damaged.
Optimize Each Laser Within Its Supported Process Window
A fair comparison does not necessarily mean forcing every laser to use identical operating settings. Different models may have different rated frequency ranges, pulse characteristics, and output behavior. Applying the same nominal frequency, software power percentage, and scan speed across all machines could unfairly disadvantage one system.
Instead, optimize each candidate within its supported range to meet the same acceptance criteria. Record the installed source model, optics, marking field, focus conditions, pulse frequency, scan speed, hatch spacing, and number of passes where relevant.
If the objective is to isolate laser-source power, control other influential conditions as closely as practical. If the objective is to choose between complete machines, compare their best validated production-ready configurations and document significant hardware differences. A complete-machine comparison can establish which configuration suits the task, but not necessarily that wattage alone caused the result.
Compare Quality, Repeatability, and Complete Cycle Time
Do not base a purchase decision on a single successful mark. Use repeated samples under representative working conditions. Depending on the application, inspect text readability, code verification, contrast, uniformity, surface damage, and any required durability after handling.
| Elemento de registro | What to document |
|---|---|
| Pieza de trabajo | Material grade, batch, color, coating, thickness, and relevant geometry |
| Requisito de marcado | Artwork or code, size, location, and acceptance criteria |
| Configuración de la máquina | Source model, optical system, field size, cooling, and relevant installed functions |
| Process settings | Frequency, scan speed, passes, focus, and other relevant parameters |
| Calidad del marcado | Pass/fail outcome, readability, visual defects, and required durability checks |
| Processing time | Laser-only marking time and complete production cycle time |
| Repetibilidad | Results across repeated samples and relevant production variation |
| Decisión final | Whether the configuration meets quality, throughput, and cost requirements |
Compare candidates using accepted output, not the maximum speed at which they can produce any visible mark. If a higher-powered system improves production performance, the gain must still justify the complete-machine configuration and cost.
For further preparation, see the lista de verificación de la prueba de marcado de muestras.
How to Make the Final 3W, 5W, or 10W Selection
The final decision should follow validated marking requirements rather than a fixed rule that every buyer must progress from 3W to 5W and then to 10W.
- Choose a suitable 3W configuration when it meets the specified quality, cycle time, repeatability, and production-margin requirements. There is no automatic need to upgrade.
- Choose a suitable 5W configuration when testing shows a meaningful improvement in accepted processing efficiency or operating margin that justifies its additional cost.
- Consider a 10W configuration when a verified power-related throughput or processing limitation makes the additional output useful and the marking quality remains acceptable.
- Reconsider the process instead of increasing power when results are limited by material response, focus, optics, positioning, or excessive surface damage.
Some projects justify testing 10W alongside a lower-power candidate from the beginning. The sequence is not mandatory; the acceptance criteria are.
For a useful machine recommendation, prepare representative workpieces or material specifications, marking artwork, marking area, target result, production quantity, and available cycle time. A supplier can then review appropriate source and machine configurations and validate samples before purchase.
Explore the available Máquinas de marcado láser UV o request an application-based quotation with your marking requirements.
Frequently Asked Questions About 3W, 5W, and 10W UV Lasers
Is a 10W UV Laser Marking Machine Always Water-Cooled?
Do not assume the cooling configuration from wattage alone. Many industrial 10W UV laser sources, including the published JPT SEAL models referenced above, use water cooling, but the required method must be confirmed for the exact source and complete machine. Lower-power UV sources can also be water-cooled, while some 3W and 5W models are air-cooled.
Is UV Laser Output Power the Same as Machine Power Consumption?
No. A 3W, 5W, or 10W rating generally refers to the laser’s optical output power under specified conditions, not complete-machine electricity consumption. Total consumption also depends on the source electronics, power supply, controller, computer, cooling system, and installed equipment. Request the complete machine’s electrical specifications when assessing operating costs or installation requirements.
Can a 3W UV Laser Marking Machine Be Upgraded to 5W or 10W Later?
An upgrade may be possible, but it is not necessarily a simple source replacement. A new laser source must be compatible with the power supply, controller, optical arrangement, cooling, mounting structure, and safety provisions. Recalibration and sample validation may also be needed. If future upgrading matters, ask the supplier whether the proposed platform supports the intended configuration and whether the change would be technically and economically reasonable.