Resource / safety and compliance
Laser Marking Machine Safety & Compliance
A laser marking machine has to be evaluated in three ways at once: as laser equipment, as a material process and, for international buyers, as an imported product. Zhuorui Laser helps buyers review laser classification, guarding, fume extraction, material hazards and destination documentation before production release.
- Laser class and beam containment
- Interlocks, access and emergency stop
- Extraction and material hazard review
- Import and documentation readiness
The direct answer
Safety is a configuration and site decision
The same laser source can require a different control strategy when the enclosure, workpiece, workflow, material or destination changes. The useful question is not “is this machine safe?” but “which hazards are controlled, by which feature, under which operating conditions?”
- Laser classification: identify wavelength, source route, accessible-emission condition and the delivered enclosure before relying on or documenting a laser classification; the applicable classification method still controls the final class.
- Beam containment: review fixed guarding, viewing protection, apertures, service access, interlocks and abnormal-stop behavior as one system.
- Process hazards: match extraction, filtration, housekeeping and fire controls to the material, coating, oil, ink, adhesive or polymer being processed.
- Site readiness: confirm utilities, grounding, operator access, local risk assessment, training, signage and maintenance responsibilities.
- Destination documentation: align labels, manuals, declarations, electrical details, packaging and import records with the receiving country and order scope.
Complete hazard map
What hazards should a laser marking machine safety review cover?
Laser radiation is only one part of the review. A useful machine-safety discussion also checks motion, electrical conditions, fire potential, process emissions and the tasks people perform during setup, production and service.
| Hazard family | Typical question | What to review |
|---|---|---|
| Laser radiation | Can direct, reflected or otherwise accessible laser radiation reach a person during operation, maintenance or service? | Wavelength, accessible emission, apertures, enclosure, viewing protection, interlocks, alignment and service access. |
| Mechanical and motion | Can moving doors, Z axes, rotary devices, conveyors or fixtures create pinch, crush or unexpected-motion hazards? | Moving parts, access zones, stopping behavior, restart logic, guarding and task sequence. |
| Electrical | Are power, protective earth, isolation and electrical access suitable for the delivered machine and installation site? | Supply voltage and frequency, grounding, cabinet access, isolation points, cables, connectors and site utilities. |
| Fire and hot particles | Can the laser process ignite the workpiece, residue, dust, packaging or nearby combustible material? | Material behavior, hot particles, unattended running, housekeeping, extraction path and local fire controls. |
| Fumes and particles | What does the actual substrate, coating, adhesive, oil or additive release when processed? | SDS, exact material grade, coating stack, capture point, extraction, filtration, filter maintenance and disposal. |
| Operation, maintenance and site | Does the risk change during loading, focusing, cleaning, troubleshooting, abnormal stops or service? | Task ownership, training, access control, PPE where required, maintenance procedure, signage and local risk assessment. |
Use this as a screening map, not a certification checklist. The controls and documentation required for a specific machine depend on the actual configuration, process, destination and installation conditions.
Standards and compliance roles
Which safety and compliance framework answers which question?
Laser classification, machine safety, workplace controls and market-entry compliance overlap, but they are not interchangeable. Buyers should know which question each framework is being used to answer.
| Framework | It mainly answers | What not to assume |
|---|---|---|
| IEC 60825-1 | How a laser product is classified and which laser-product safety requirements apply to accessible laser radiation. | A classification by itself does not complete the full workplace, process or destination review. |
| ISO 11553-1:2020 | Laser-radiation safety requirements and manufacturer information for laser processing machines, in addition to IEC 60825 requirements. | It should not be treated as a substitute for every other machinery, electrical, fire, process or site requirement that may apply. |
| Workplace / site safety (U.S. OSHA example) | How the installed laser is controlled during actual operation, maintenance and service, including engineering, administrative and PPE controls as applicable. | A supplier document does not replace the receiving site’s own duties, procedures or local risk assessment. |
| EU conformity / CE route | Which applicable EU legislation, conformity assessment, technical documentation, declaration and CE-marking responsibilities apply before the product is placed on the EEA market. | A CE mark is not a shortcut around identifying the applicable legislation and assessing the actual product. |
| U.S. FDA laser-product requirements | Which U.S. federal laser-product performance, reporting and related requirements apply; FDA guidance also explains its approach to IEC 60825-1 Edition 3 conformance. | IEC conformity should not be assumed to be identical to every FDA requirement. |
Practical takeaway: Class 1, CE marking, FDA requirements and workplace safety are different questions. A complete review connects them to the same delivered machine and operating conditions rather than treating any one label as the whole answer.
Safety & compliance guides
Choose the right laser safety and compliance guide
Start with the risk you need to resolve. The specialist guides go deeper into individual questions; this page keeps the overall machine, site and destination picture together.
- Laser Safety Classes Explained: use this when you need the Class 1/Class 4 and complete-system classification boundary.
- Open vs Enclosed Laser Marking Safety: use this when selecting a guarding strategy or comparing open and enclosed workflows.
- Laser Safety Glasses Selection: use this when eyewear may be required for the installed wavelength and exposure condition.
- Fume Extraction Guide: use this when fumes, particles, filtration, airflow or maintenance are part of the process risk.
- PVC and Halogenated Plastic Risks: use this before testing or processing PVC, halogenated or uncertain polymer formulations.
- CE, FDA and Laser Compliance Overview: use this when the key question is market-specific conformity, documentation or importer responsibility.
Laser class education
Laser safety classification follows accessible emission, not marketing shorthand
Class labels depend on the accessible emission of the complete delivered product and the applicable classification method. Use the matrix as a buyer checklist, then verify the actual source, enclosure and label for the ordered configuration.
Reference basis: OSHA laser-safety guidance evaluates accessible emission together with protective housing and interlocks, while the U.S. FDA regulates laser products under 21 CFR 1040.10 and 1040.11 and recognizes specified IEC 60825-1 Edition 3 provisions through Laser Notice 56. OSHA laser safety guidance · FDA Laser Notice 56
| Review point | What to ask | Control implication | Evidence to request |
|---|---|---|---|
| Enclosed, inaccessible beam path | Is the beam path fully contained during normal operation, with no unintended aperture or bypass? | Interlocked access, viewing protection, service mode and abnormal-stop behavior must be reviewed. | Delivered enclosure description, access points, interlock logic and product label. |
| Open or service-access condition | Can an operator or technician access direct or reflected radiation during setup, alignment or maintenance? | Controlled access, documented procedure, trained personnel, appropriate eyewear and local rules may apply. | Service procedure, hazard assessment, wavelength and eyewear specification where applicable. |
| Source and wavelength | What wavelength and source are installed in the quoted configuration? | Invisible near-infrared or ultraviolet emission cannot be judged by visible brightness; reflection and skin/eye hazard require controls. | Source model, wavelength, installed power range and configuration revision. |
| Class label and destination rules | Which classification and marking requirements apply in the receiving market? | Labels, manuals, declarations and site controls should match the actual product and destination. | Product label artwork, technical file references and destination compliance checklist. |
Guarding and access
Review laser guarding, interlocks and operator access together
Guarding has to work during the tasks people actually perform, not only during automatic marking. Review loading, focusing, cleaning, maintenance, troubleshooting and abnormal stops because each can create a different access condition.
Map the task
List loading, positioning, focusing, marking, verification, unloading, cleaning and service actions.
Identify exposure
Consider direct beam, specular reflection, diffuse reflection, motion, pinch points and hot or sharp parts.
Check controls
Review enclosure, interlocks, emergency stop, key or access control, signage and restart behavior.
Review service mode
Separate normal operation from alignment and maintenance; define who may enter and under what procedure.
Record the handoff
Keep the risk assessment, manuals, training record and delivered configuration tied to the machine.
Fumes and hazardous materials
Laser fume extraction starts with the material, coating and SDS
Laser-generated fumes and particles vary with substrate, coating, additives, oils, inks and adhesives. A visible mark is not evidence that the airborne contaminant, fire or filter-disposal risk is acceptable.
NIOSH test example: A health-hazard evaluation of laser marking on multiple substrates identified material-dependent airborne contaminants. Under the tested conditions, PVC marking generated compounds including hydrochloric acid and vinyl chloride, while the evaluated exhaust ventilation controlled the contaminants generated during those trials. NIOSH HETA 99-0109-2754
| Material or process | Why it needs review | Pre-test information | Control questions |
|---|---|---|---|
| Plastics and polymers | Thermal decomposition can release irritant, toxic or corrosive compounds; flammability can change with additives. | Exact grade, color, additives, coating, SDS and intended mark. | Local capture point, filter media, airflow, fire controls and disposal route. |
| PVC, halogenated or unknown materials | Unknown formulation or halogen content may create corrosive or hazardous emissions and damage extraction equipment. | Supplier SDS, formulation information and a hold point before sample testing. | Is the material approved for testing? Is filtration compatible and maintainable? |
| Paints, inks, oils and adhesives | Coatings and residues can change fume chemistry, ignition risk and surface response. | Coating stack, cure state, SDS and cleaning process. | Does the extraction capture the plume at source without disturbing the mark? |
| Metals, oxides and fine particles | Fine particulate, hot debris and reflective surfaces can affect exposure, housekeeping and fire risk. | Alloy, plating, oxide state, oil and expected mark mechanism. | Capture efficiency, spark or hot-particle controls, filter change and housekeeping. |
| Composite or layered parts | Different layers can produce different fumes, delamination or unpredictable marking behavior. | Layer stack, resin or adhesive, fiber content, SDS and sample photos. | Can the extraction and fire strategy handle the complete material stack? |
Worked decision examples
Apply the framework to the actual machine, material and workflow
These examples are not classifications or compliance determinations. They show how the same review framework changes when the laser source, enclosure, material and production method change.
Open 1064 nm fiber marking on stainless steel
Start with access, not with the material name. An open working area changes how accessible radiation, reflections and operator access must be reviewed.
- Confirm the installed source and wavelength.
- Review direct and specular-reflection paths around the fixture and workpiece.
- Define the controlled work area, access rules and eyewear requirements where applicable.
- Check loading, focusing, alignment and service tasks separately from normal marking.
- Review metal residue, coatings, oils and extraction needs for the actual part.
Enclosed 355 nm UV marking on a plastic component
Do not stop at “enclosed.” The enclosure has to be considered together with accessible emission, access points, viewing protection, interlocks and the actual polymer.
- Verify the delivered enclosure and any access-door or service conditions.
- Check whether the viewing window and access openings are appropriate for the installed wavelength.
- Review interlock and restart behavior where those controls are part of the configuration.
- Identify the exact plastic, coating, additives and SDS before relying on sample appearance.
- Match extraction and filtration to the tested material and process.
CO₂ flying marking integrated with packaging production
The laser is now part of a moving production system. Beam containment has to be reviewed together with line motion, material behavior and stop/restart conditions.
- Review the beam path and containment around the moving product.
- Define the interface between laser enable, conveyor motion, guards and production-line stops.
- Check restart behavior after jams, emergency stops or line interruptions.
- Review the packaging material for fumes, fire behavior and residue.
- Confirm the extraction point and production-site ownership before commissioning.
The decision pattern is the same: identify the actual source and accessible condition, map the task, review the material/process hazard, confirm the control strategy, then document what belongs to the supplier, importer and receiving site.
Evidence-led review
Use the machine record as the compliance spine
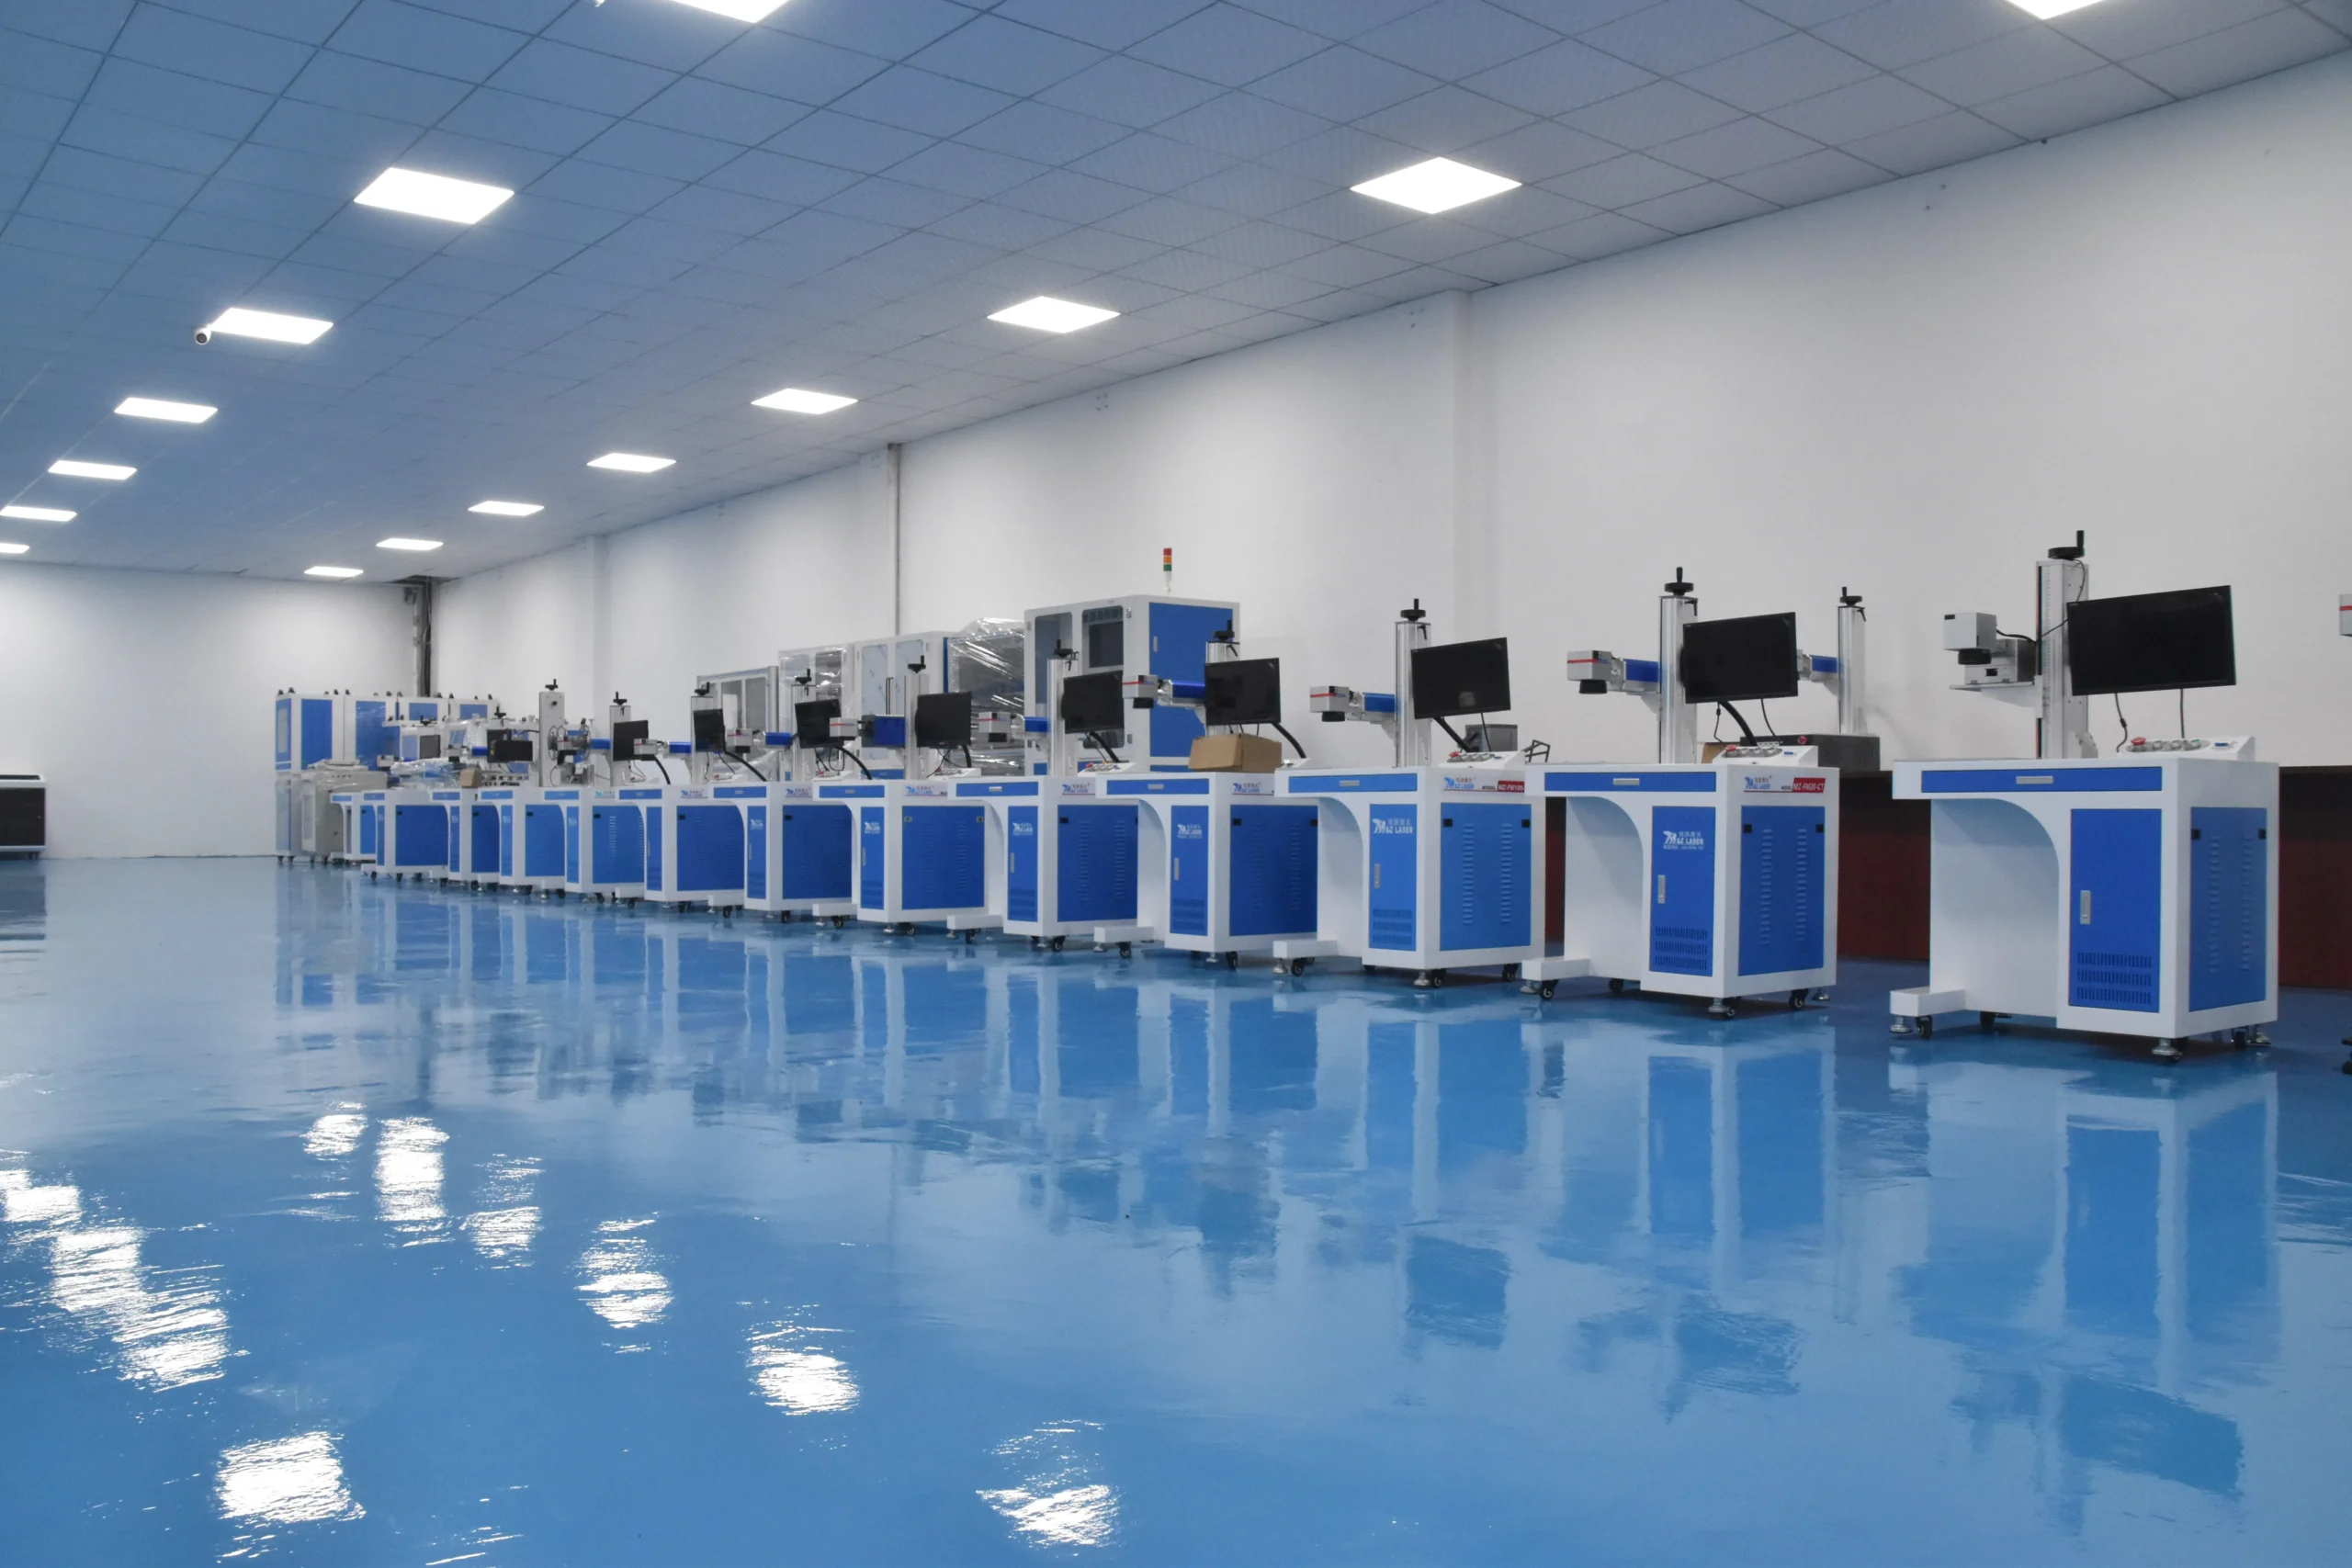
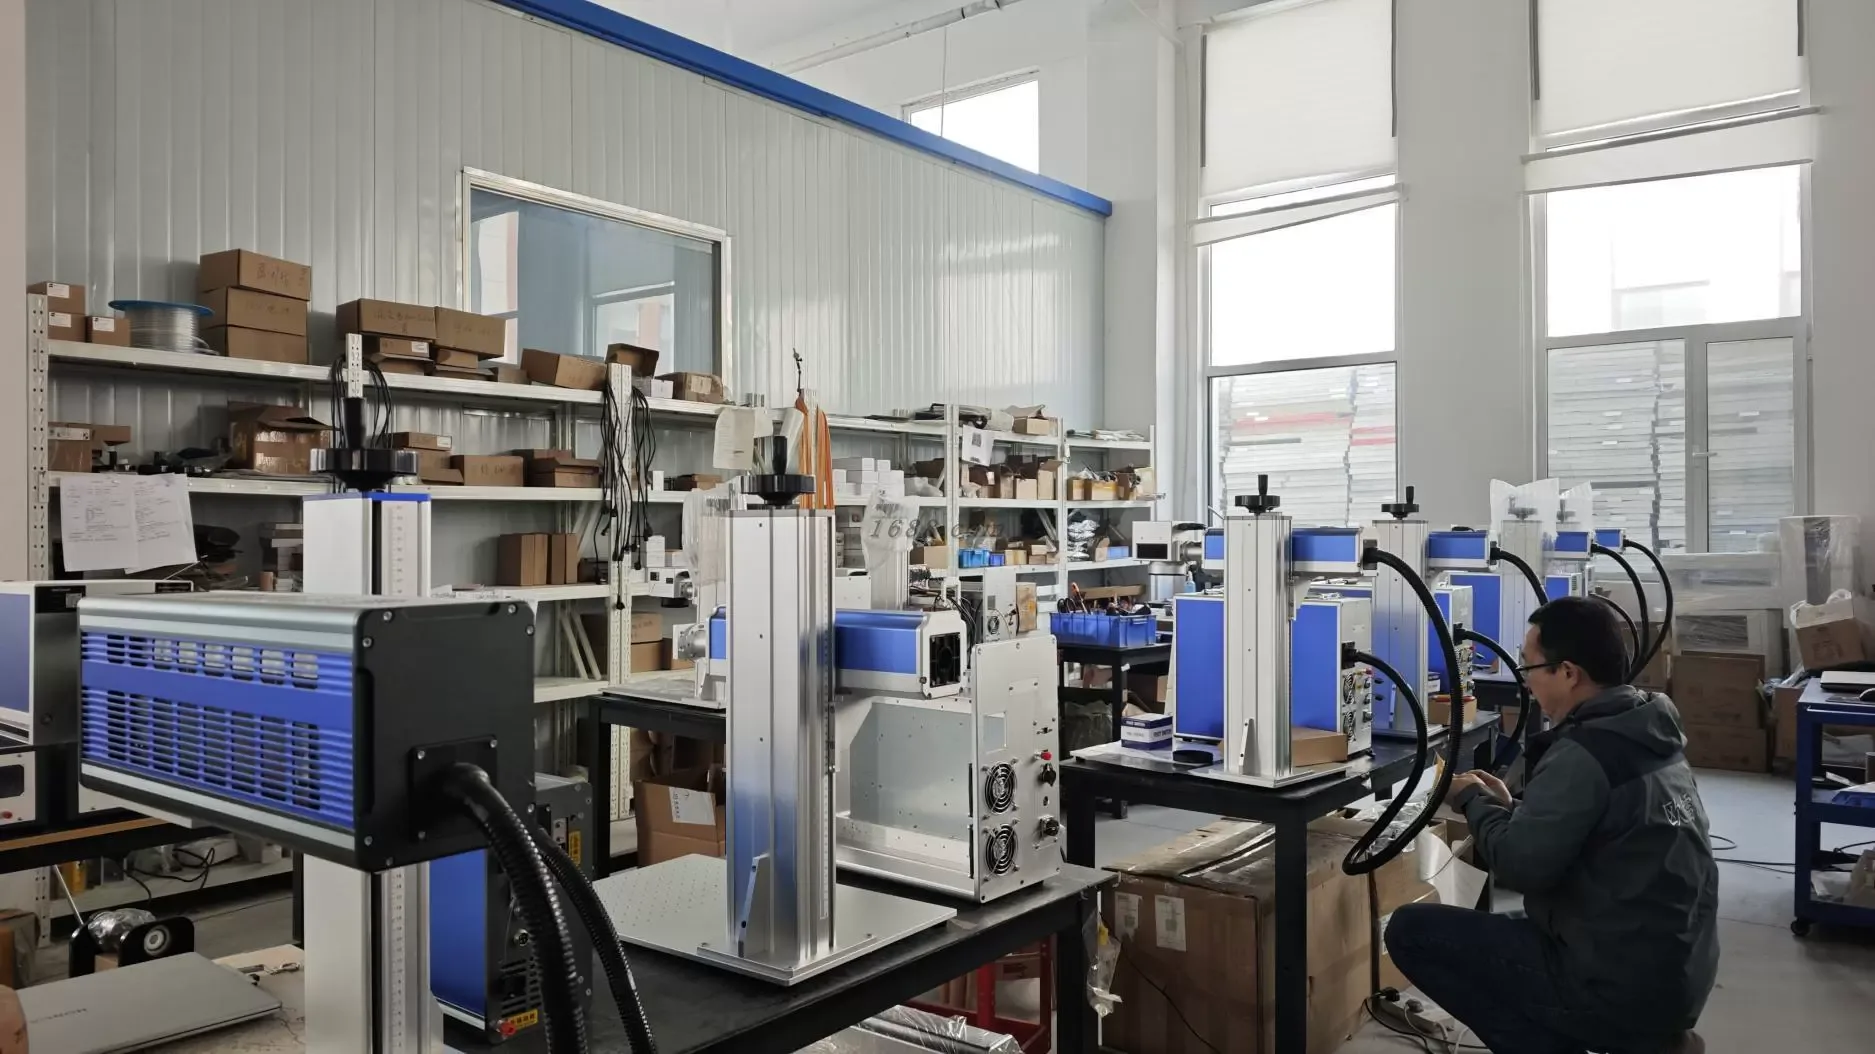
Factory and equipment images show useful context, but they do not by themselves prove that a machine is compliant. For the delivered unit, the important record is the actual configuration, safety assessment, functional test record and destination documentation.

Import and destination readiness
Confirm laser marking machine compliance documents before shipment
Before production, agree the document set for the receiving country and ordered configuration. The commercial invoice, packing list, machine identity and technical records should all describe the same delivered unit.
Regulatory context: In the EEA, CE-marking responsibilities include manufacturer conformity assessment, technical documentation and the declaration of conformity, while importers have their own verification duties. In the United States, laser products are separately subject to FDA radiation-safety requirements before entering commerce. European Commission — manufacturers · European Commission — importers · FDA market-entry FAQ
| Document or record | Purpose | What to confirm before shipment |
|---|---|---|
| Machine identity and nameplate | Links the delivered unit to the ordered configuration and serial record. | Model, serial, electrical details, source information and labels match the final machine. |
| User manual and safety instructions | Explains operation, hazards, guarding, maintenance, emergency actions and limitations. | Language, revision, destination expectations and delivered options are aligned. |
| Declarations and technical file references | Supports the applicable conformity route for the machine and receiving market. | Which declaration, standards references or local assessment are required is confirmed with the importer or compliance owner. |
| Electrical and utility information | Allows the site to verify voltage, frequency, grounding, cooling, air and extraction needs. | Quoted utilities, plugs, adapters, grounding method and site responsibilities are explicit. |
| Commercial and transport records | Supports customs entry, classification, valuation, packing and delivery handoff. | Invoice, packing list, HS-code responsibility, country-of-origin data, crate details and incoterms are agreed. |
| Packaging and restricted-material review | Reduces delays from wood packaging, batteries, chemicals or other transport restrictions. | Packaging marks, treatment records and any restricted-material declarations are supplied where applicable. |
Buyer qualification checklist
Ask for the evidence that matches your risk
Use these checkpoints during quotation review, factory acceptance testing or site-readiness planning. The exact evidence and documents depend on the machine configuration and destination.
Factory acceptance and pre-shipment review
Verify the delivered machine, not only the quotation
During FAT or pre-shipment review, check the controls and records that are part of the agreed configuration. The goal is to confirm that the machine being released matches the safety assumptions used during quotation and design review.
| Acceptance point | What to verify | Record or outcome |
|---|---|---|
| Configuration identity | The delivered source model, wavelength, machine model, key options and configuration revision match the order record. | Machine identity and configuration are traceable before release. |
| Labels and safety information | Product labels, laser warnings and operating information match the delivered configuration and agreed destination requirements. | Any mismatch is corrected or recorded before shipment. |
| Guarding and access | Where guarding, access doors, viewing protection or controlled openings are part of the machine, verify that the delivered hardware matches the approved configuration. | Physical configuration is checked against the machine record. |
| Interlocks and emergency stop | Where interlocks or emergency-stop functions are included, demonstrate the agreed response under the relevant operating condition and confirm restart behavior. | Functional-check result, deviation and owner are recorded. |
| Normal operation vs service | Confirm which tasks can expose a different access condition during focusing, alignment, cleaning, troubleshooting or service. | Manual, service instructions and access responsibilities are aligned. |
| Material and extraction interface | Confirm the intended material/process assumption, extraction connection and capture point where these were part of the agreed scope. | Supplier scope and receiving-site responsibilities are explicit. |
| Manuals and records | Check that manuals, electrical information, configuration records and agreed supplier-side documents describe the machine actually being released. | Document revision and machine identity are consistent. |
| Open deviations | List unresolved safety-function, documentation or configuration deviations before release rather than relying on verbal follow-up. | Deviation, responsible owner, due action and release status are documented. |
Acceptance testing is not a certification. A FAT or pre-shipment check does not replace formal product classification, conformity assessment, workplace risk assessment or any competent-person review required by the destination or installation site.
Clear ownership boundaries
Compliance works when every decision has an owner
For a confirmed order, Zhuorui can provide the agreed machine and configuration information together with the supplier-side documents available for that configuration. Site approval, importer duties and local authorization remain with the responsible buyer, importer and site parties.
Zhuorui owns
Confirm in the order which supplier-side items are included: configured machine information, agreed safety features, manuals, labels, test records and shipment documents as applicable.
Buyer or importer owns
Destination requirements, customs entry, local conformity route, competent-person review and site authorization.
Site owner owns
Workplace risk assessment, utilities, extraction installation, training, maintenance controls and local operating rules.
Material owner owns
Accurate SDS, formulation and coating information, approval of the process result and safe handling of generated waste.
Safety and compliance FAQ
Questions buyers ask before importing a laser marker
Use these answers to identify what still needs to be checked for the actual machine, material and destination. The written order and local requirements determine the final responsibilities.
Does an enclosed laser marking machine automatically mean Class 1?
No. Classification depends on the accessible emission of the complete delivered product and the applicable classification method. An enclosure can be an important control, but the source, apertures, service mode, interlocks and actual configuration still need to be assessed.
Are laser safety glasses enough to make an open machine safe?
No. Eyewear is only one possible administrative or personal-protection control. Beam containment, access control, interlocks, emergency stop, procedures, training and a competent-person risk assessment remain central. Eyewear selection must match the installed wavelength and the protection level required by the risk assessment; appearance alone is not sufficient.
Can I test an unknown plastic or PVC sample?
Do not assume it is acceptable. Obtain the exact material and SDS first, check for PVC, halogens, flame retardants, unknown additives or coatings, and review extraction, corrosion, fire and waste controls before testing. A sample hold is appropriate when the formulation is not known.
Does Zhuorui provide CE or other destination certification?
The applicable conformity route and document set depend on the destination, importer role and delivered configuration. Zhuorui can prepare the supplier-side machine information and agreed documentation for the confirmed order. Any declaration, certification, registration or filing must be confirmed for the exact configuration and destination before shipment; the importer or local compliance owner remains responsible for its own legal obligations.
What import documents should be agreed before shipment?
At minimum, align the machine identity, invoice, packing list, electrical and utility data, manuals, labels, applicable declarations, country-of-origin information, packaging records and the party responsible for customs classification and entry. Add language, wood-packaging or restricted-material records when the route requires them.
Can a successful sample mark prove the machine is compliant?
No. A sample result addresses process direction and acceptance criteria. Compliance also requires the correct guarding, controls, extraction, documentation, installation and site responsibilities for the delivered machine and destination.
Next step
Bring the safety and import brief into the quotation
Send the target material and SDS, laser route if known, machine format, production workflow, destination country, required language, extraction expectations and any buyer or importer checklist. Zhuorui can use this information to review the machine configuration and confirm which supplier-side documents are available for the order.
Useful inputs: material and SDS / target mark / source or wavelength / machine format / enclosure and workflow / extraction / destination and importer / language / required documents / acceptance method.