Laser Marking Comparison Guides
Compare laser marking technologies, marking mechanisms and non-laser alternatives before a machine specification is written. Start with the material, required mark, production method and acceptance test, then use the relevant guide to compare the options in detail.
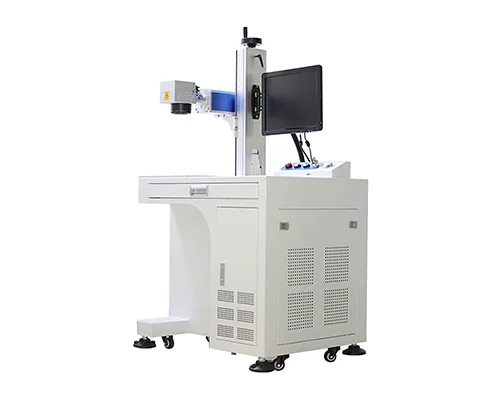
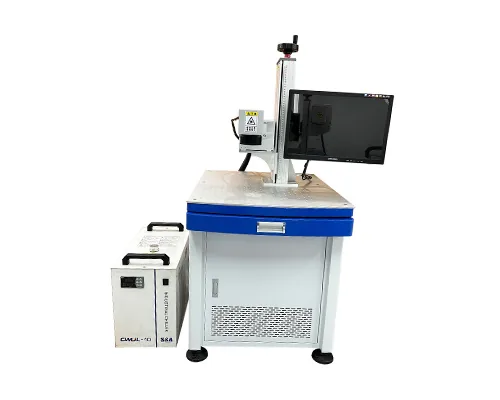
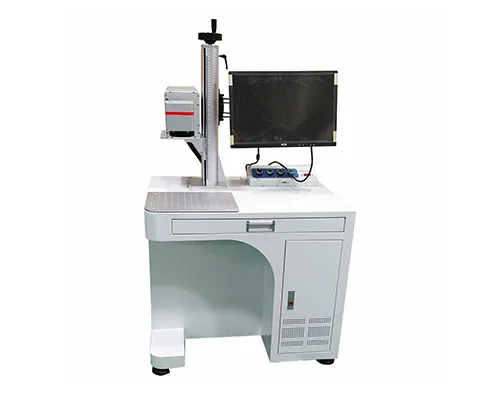
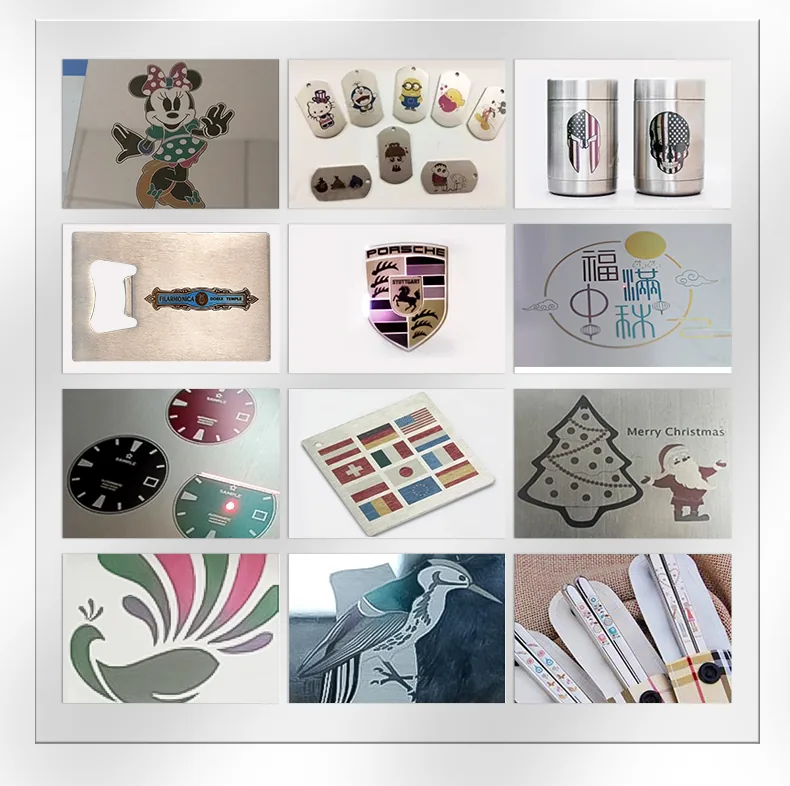
Representative Fiber, UV and CO2 equipment images. They show the equipment families only; actual marking results still depend on the sample and machine configuration.
Choose Your Laser Marking Comparison Path
Do not begin with wattage or machine price. First decide whether the unresolved question is the laser source, the physical mark, or a different coding process. Each path below leads to a focused technical guide.
Choose a laser source
Compare wavelength family, material response, heat input, pulse behavior, mark effect and practical operating constraints.
See four source comparisonsDefine the physical result
Separate surface marking from material-removal engraving and chemical or electrochemical etching before discussing equipment.
Compare marking, engraving and etchingCompare another coding process
Evaluate permanence, contact, consumables, maintenance, line integration and inspection against dot peen or inkjet.
See alternative-process guidesFiber, MOPA, UV or CO2: Where Should You Start?
Use this as a screening table, not a material approval. The same material name can respond differently because of grade, additives, coating, color, geometry and the required mark.
| Decision point | Fiber | MOPA fiber | UV | CO2 |
|---|---|---|---|---|
| Technology position | Pulsed fiber-laser route commonly evaluated for industrial marking on metals and selected plastics. | A pulsed fiber architecture with wider pulse-control flexibility than many conventional Q-switched sources; it is not a separate wavelength family. | Short-wavelength route commonly evaluated when fine features, surface sensitivity or lower thermal influence matter. | Longer-wavelength route commonly evaluated for many organic, packaging and other non-metal surfaces that absorb CO2 radiation well. |
| Good first question | Does the part need permanent metal identification, engraving or high-throughput marking? | Is a fiber route already suitable, but pulse width, heat input or surface effect still needs more control? | Is the substrate heat-sensitive, finely featured, coated or difficult to mark cleanly with a fiber route? | Is the target paper, wood, leather, polymer, coating or packaging surface where CO2 absorption is favorable? |
| What can change the answer? | Alloy, finish, coating, additives, required depth, field size and cycle target. | Source architecture, available pulse-width range, frequency/energy window, surface finish and required visual effect. | Actual formulation, transparency, coating stack, feature size, damage threshold and cycle requirement. | Exact substrate or coating, absorption, mark mechanism, extraction, line speed and maintenance context. |
| Main caution | “Metal” or “plastic” alone is not enough to approve the process. | Do not assume MOPA automatically produces color, better contrast or less heat on every part. | “Cold marking” is not zero-heat processing, and UV is not automatically the best route for every plastic or glass part. | Do not assume bare-metal marking or a specific contrast result without testing the real surface. |
Use the table to choose a test direction. Final selection should still be based on the real part, mark file, production target and acceptance criteria.
Four Manufacturing Tasks and the Comparison Route to Open First
These are practical starting points, not guaranteed machine selections. Their purpose is to translate engineering variables into recognizable production situations.
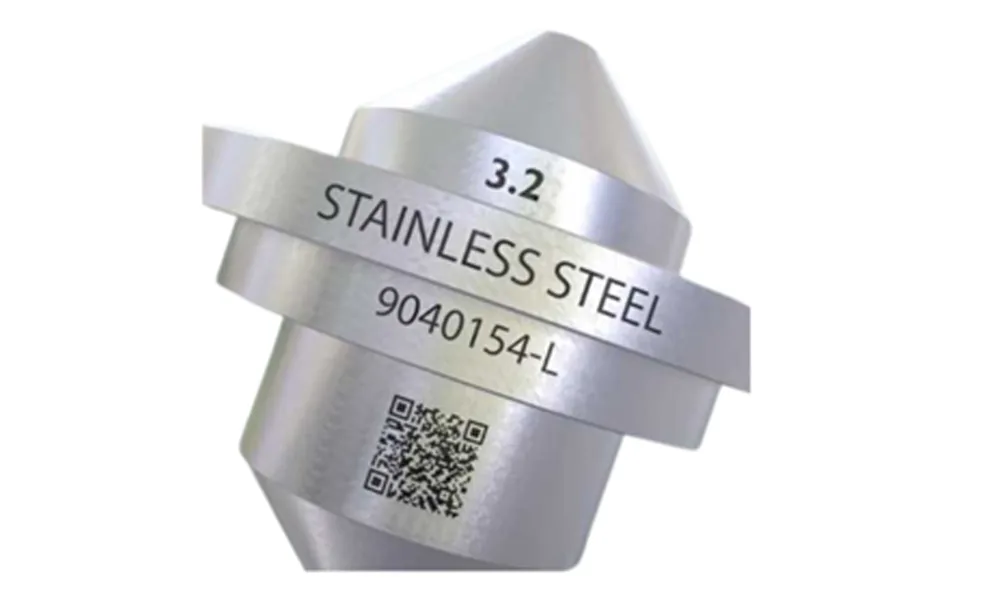
Start with fiber. Compare MOPA when pulse flexibility, color development, heat input or a wider process window matters. Validate readability, surface condition and cycle time on the real part.
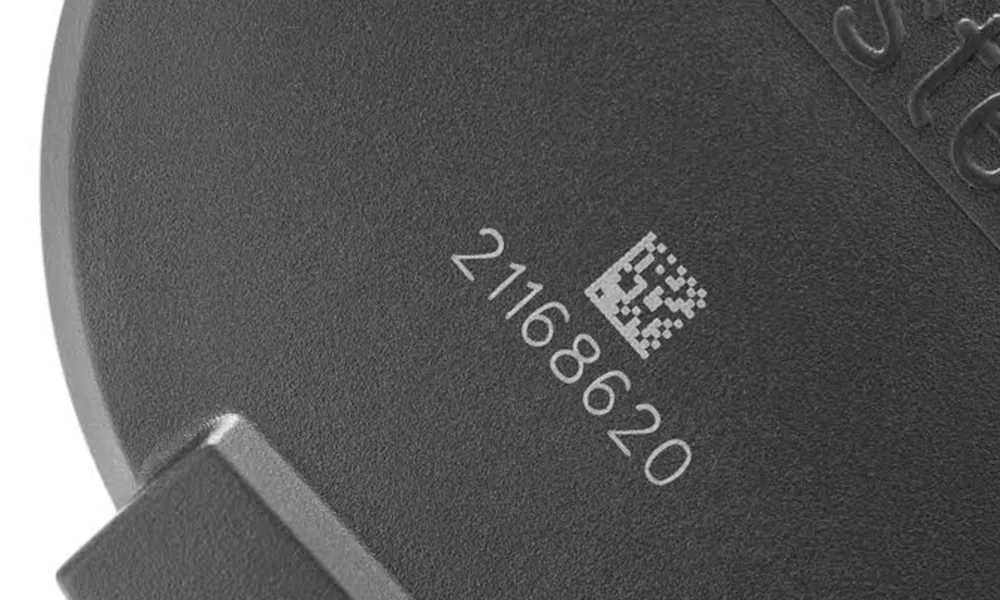
Compare fiber and UV on the actual polymer formulation. Pigments, fillers, additives and color can change absorption, contrast and damage risk, so the resin name alone is not enough.
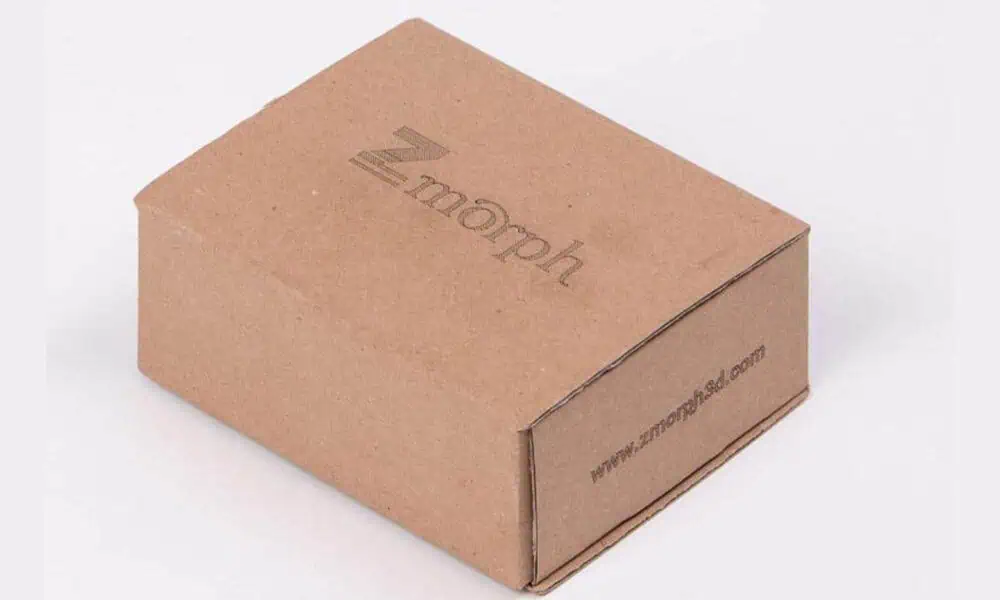
Compare UV and CO2 where the substrate can respond to either route. If the line also uses inkjet, include consumables, cleaning, ventilation, code verification and changeover in the comparison.
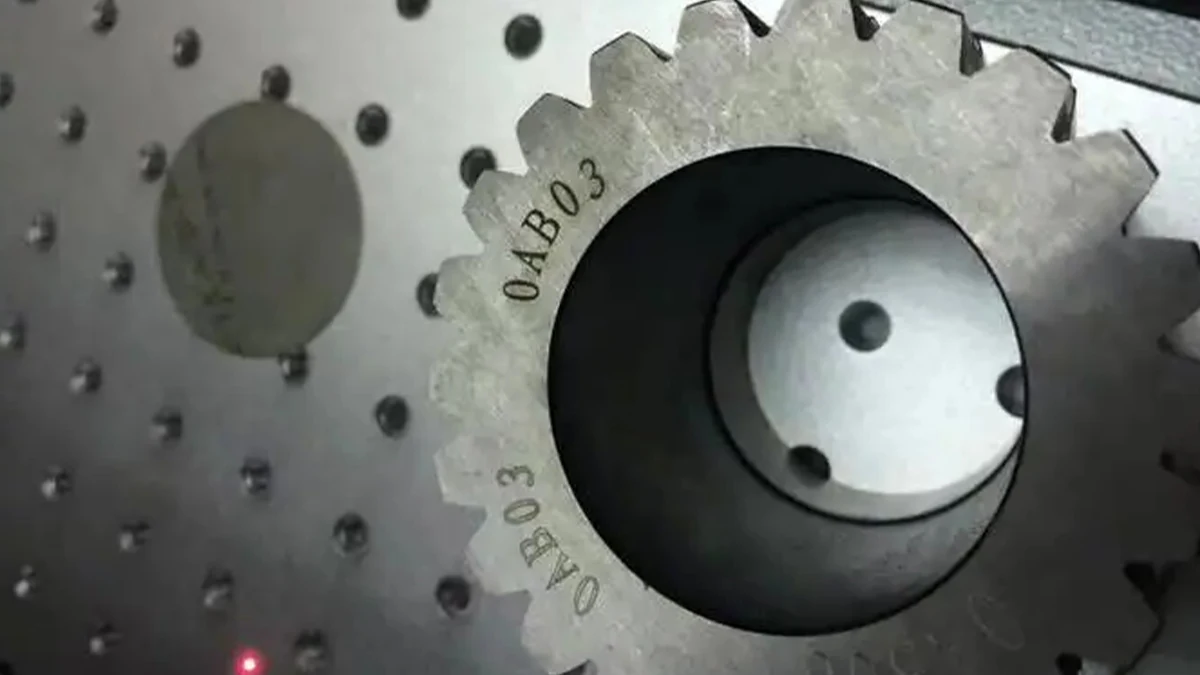
Compare laser engraving with dot peen when depth and permanence matter. Check allowed deformation, part stiffness, mark depth, noise, tooling access, cycle time and code-quality requirements.
Compare Fiber, MOPA, UV and CO2 Laser Marking Options
Choosing a source family narrows the options, but it does not confirm that the process will work on a specific part. Surface condition, additives, coatings, geometry, field size, focus, pulse settings and the acceptance test can change the practical result.
Compare Laser Marking with Engraving, Etching, Dot Peen and Inkjet
Two systems can produce readable characters while creating very different surface changes, maintenance tasks and validation requirements. Before comparing equipment, define what the mark must still meet after cleaning, wear, heat or chemical exposure.
First-Pass Process Comparison
Before comparing machine models, separate how the mark is created. Surface marking, deliberate material removal, mechanical indentation and deposited ink create different durability, maintenance and inspection requirements.
| Decision point | Laser surface marking | Laser engraving / etching | Dot peen | Inkjet coding |
|---|---|---|---|---|
| How the mark is formed | Non-contact laser interaction changes color, chemistry or surface appearance with little or no intentional depth. | Laser energy intentionally removes or modifies material to create a recessed or textured mark; exact “etching” terminology should be defined for the application. | A stylus mechanically indents the surface. | Ink is deposited onto the surface. |
| Part deformation / material removal | Usually low, but thermal or surface effects still require validation. | Material removal or measurable surface change is part of the intended result. | Mechanical deformation is inherent to the process. | No intentional substrate removal; adhesion and drying become key variables. |
| Consumables / wear items | No ink or stylus is consumed at the mark point; extraction filters and normal maintenance may still apply. | Similar laser-system maintenance, with added attention to debris and extraction when material is removed. | Stylus/tool wear and mechanical maintenance are part of the process. | Ink, make-up/solvent and cleaning requirements are central operating variables. |
| Open this comparison when… | You need permanent, non-contact identification with controlled visual or surface change. | Depth, tactile result, roughness or material removal is part of the specification. | Permanent recessed identification may justify controlled mechanical indentation. | High-speed coding can use a deposited mark and consumable management is acceptable. |
Clarify whether the target is a surface color or texture change, deliberate material removal, or an etching mechanism. Depth, roughness, debris, corrosion behavior and dimensional limits are different questions.
Open the terminology and mechanism guideCompare non-contact processing with permanent mechanical indentation. Part stiffness, surface deformation, noise, tool wear, data needs and readable depth belong in the decision.
Open the laser vs dot peen guideCompare a laser-created mark with deposited ink. Substrate response, contrast, line speed, changeovers, consumables, cleaning, ventilation and code verification should be evaluated together.
Open the laser vs inkjet guideChoose the Right Laser Marking Comparison Guide
| Starting condition | Open this guide first | Bring these variables |
|---|---|---|
| Metals and selected plastics; UV is also under review | Fiber vs UV | Alloy or polymer grade, surface finish, contrast target, feature size, heat limit and throughput. |
| Metal-focused route compared with organic or coated surfaces | Fiber vs CO2 | Material family, coating stack, required mechanism, field size, extraction and maintenance context. |
| Fine or heat-sensitive processing compared with CO2-responsive materials | UV vs CO2 | Surface absorption, damage threshold, mark detail, packaging or organic material condition and cycle target. |
| A fiber route is selected, but pulse flexibility is unresolved | MOPA vs Q-switched | Required color or contrast, pulse-width need, mark speed, source range and sample acceptance method. |
| The requested result is described inconsistently | Marking vs engraving vs etching | Target depth, roughness, material removal, surface integrity, corrosion or cleaning requirement. |
| Permanent industrial identification may use mechanical indentation | Laser vs dot peen | Part stiffness, permitted deformation, required depth, noise, tool access, data and maintenance. |
| A production line currently uses or considers deposited ink | Laser vs inkjet | Substrate, ink adhesion, consumables, cleaning, line speed, code verification and ventilation. |
Use One Evidence Method for Every Comparison
A useful comparison keeps the sample and acceptance test constant. Otherwise the result may reflect a different material condition, mark file or production target rather than a better process route.
- 1
Freeze the part condition
Record material grade, color, finish, coating, contamination, wall thickness and geometry.
- 2
Define the required mark
Provide the file, size, line width, code type, contrast, depth, texture and protected areas.
- 3
Compare the production system
Include loading, fixture, focus control, cycle target, extraction, guarding, software and verification.
- 4
Approve with a repeatable test
Set the inspection lighting, reader, cleaning, abrasion, heat, chemical or dimensional acceptance method.
Laser marking comparison questions
Use these answers as a starting point. The detailed guide and a controlled sample test should confirm the final choice.
Which laser marking technology is best?
There is no universal best source. The practical choice follows material and surface response, required mark effect, geometry, cycle target, integration, safety controls and the acceptance test. Use the source comparisons to narrow the test route.
Is MOPA a separate laser family from fiber?
MOPA is a type of pulsed fiber-laser architecture, not an unrelated wavelength family. Compare it with a conventional Q-switched fiber source when pulse-width flexibility or selected color and contrast effects matter.
Does higher wattage make one route better?
No. Rated power alone does not define absorption, peak power, pulse behavior, spot size, heat input, mark quality or cycle time. Compare the complete source, optics, settings and sample result.
When should dot peen be compared with laser marking?
Compare them when permanent industrial identification could accept mechanical indentation. Required depth, surface deformation, part stiffness, noise, tool wear, access and data workflow are central variables.
When should inkjet be compared with laser marking?
Compare them when a line can use deposited ink or a laser-created mark. Review substrate compatibility, contrast, consumables, cleaning, changeover, line speed, ventilation, maintenance and verification together.
Can a comparison guide replace sample testing?
No. A guide can identify the most suitable route to test first, but it cannot confirm contrast, damage, adhesion, depth, durability, code grade or cycle time on an unseen production part.
Prepare a Testable Laser Marking Brief
Zhuorui Laser supplies standard machines, supports function upgrades and custom machine configurations, and can evaluate project-based automation requirements. A recommendation is more reliable when you provide the actual part, marking requirement, production conditions and acceptance criteria before quotation.
Test the Route Before Selecting the Machine
Share the material, surface condition, mark file, production target and pass/fail method. Zhuorui Laser can then recommend a source, configuration and sample-test plan based on the real application rather than the comparison table alone.